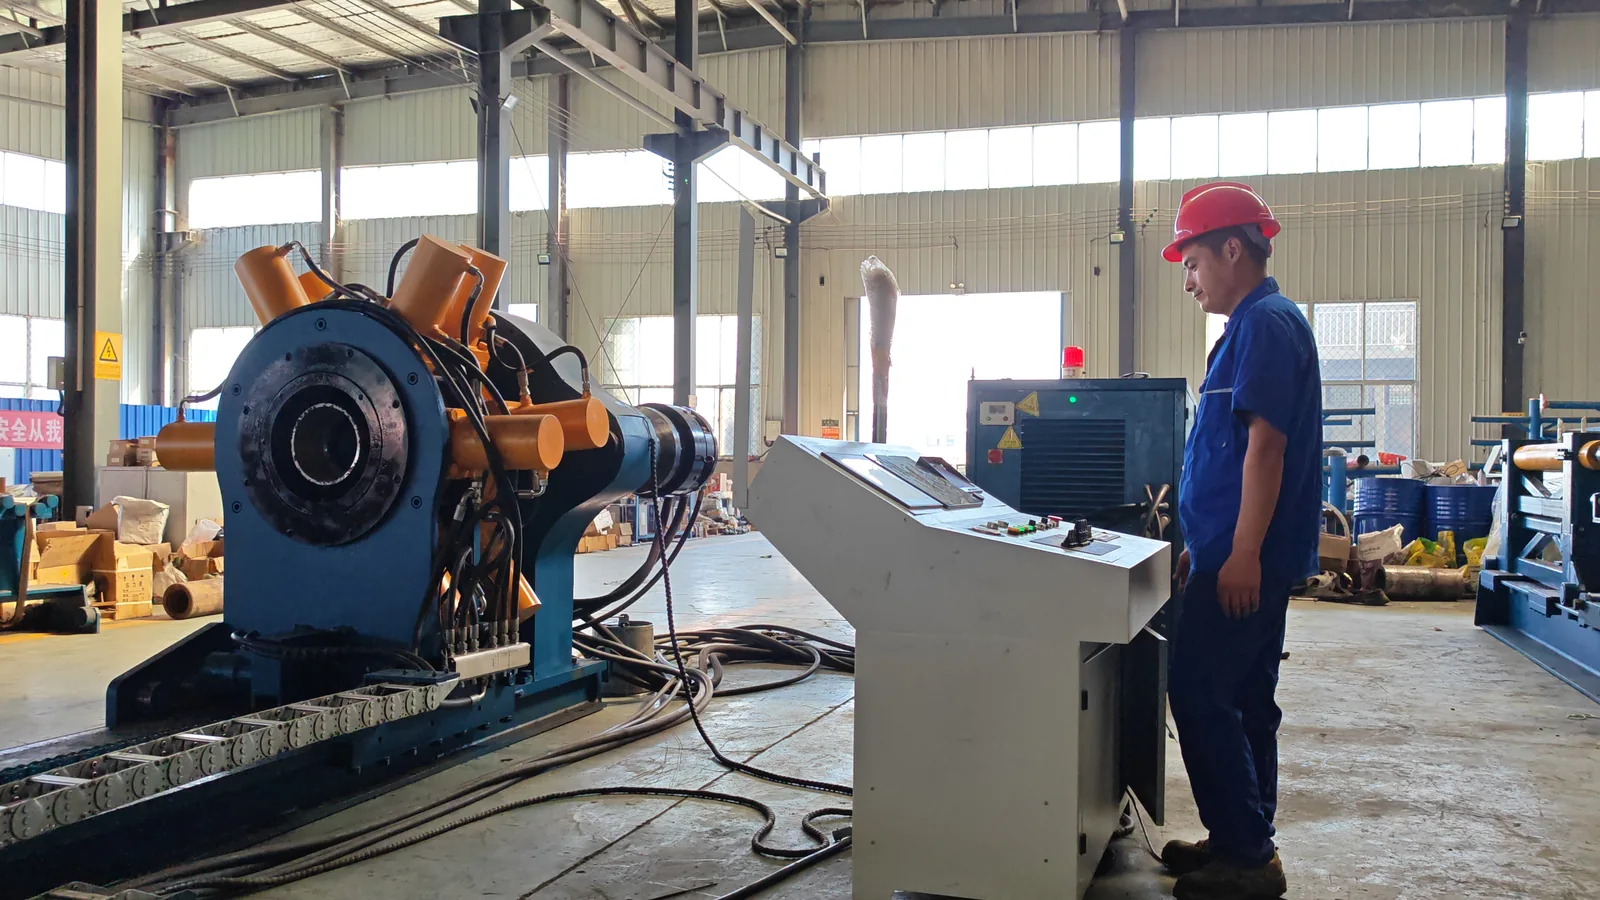


Bucking unit specifications: grip, torque and speed
The reference frames run from 10 to 24 in. Start with the smallest and largest gripping diameters, then check the required torque and the length and weight of the assembly. The tables show which published ranges belong to each frame; the quotation confirms the supplied configuration.
Specifications reviewed 16 September 2026.
TorqueStar torque-turn software
TorqueStar brings connection settings, live torque-turn monitoring and make-up reports into one workflow. Select the connection, follow make-up, then review the result.
Beckhoff PLC controls
Beckhoff PLC controls the machine; TorqueStar handles connection settings and job records. The quotation confirms the controller model, software functions and manual or automatic operating steps.
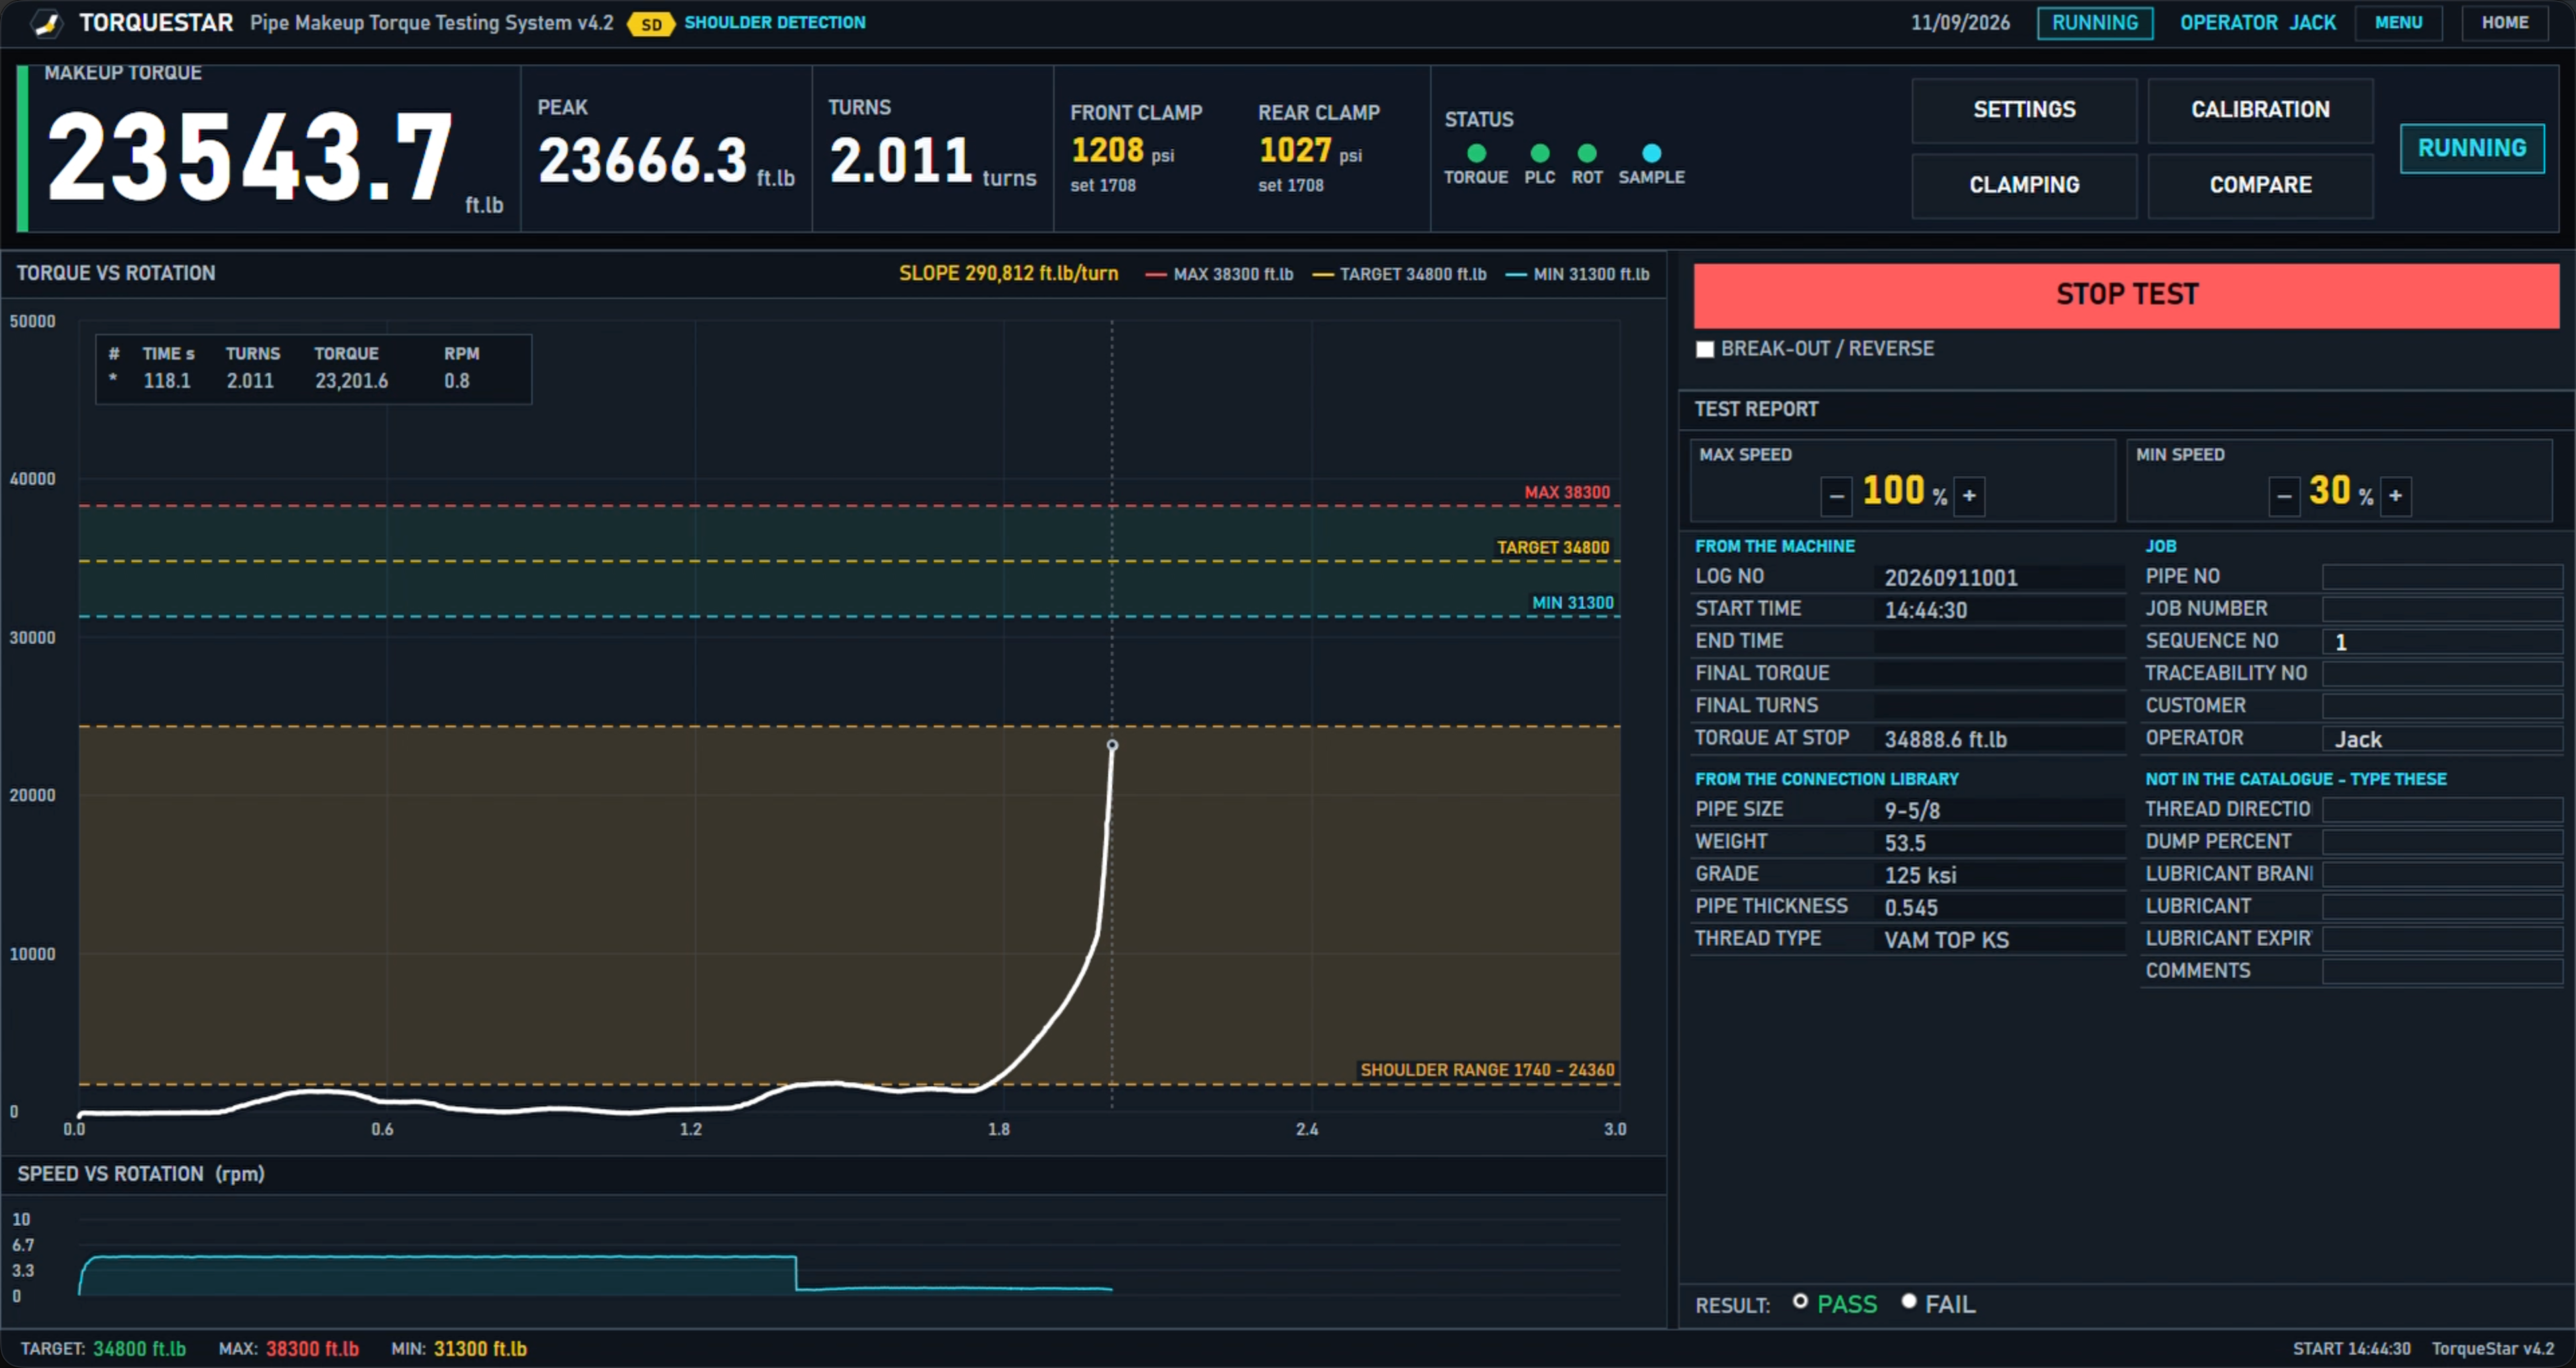
Open monitoring screen ↗
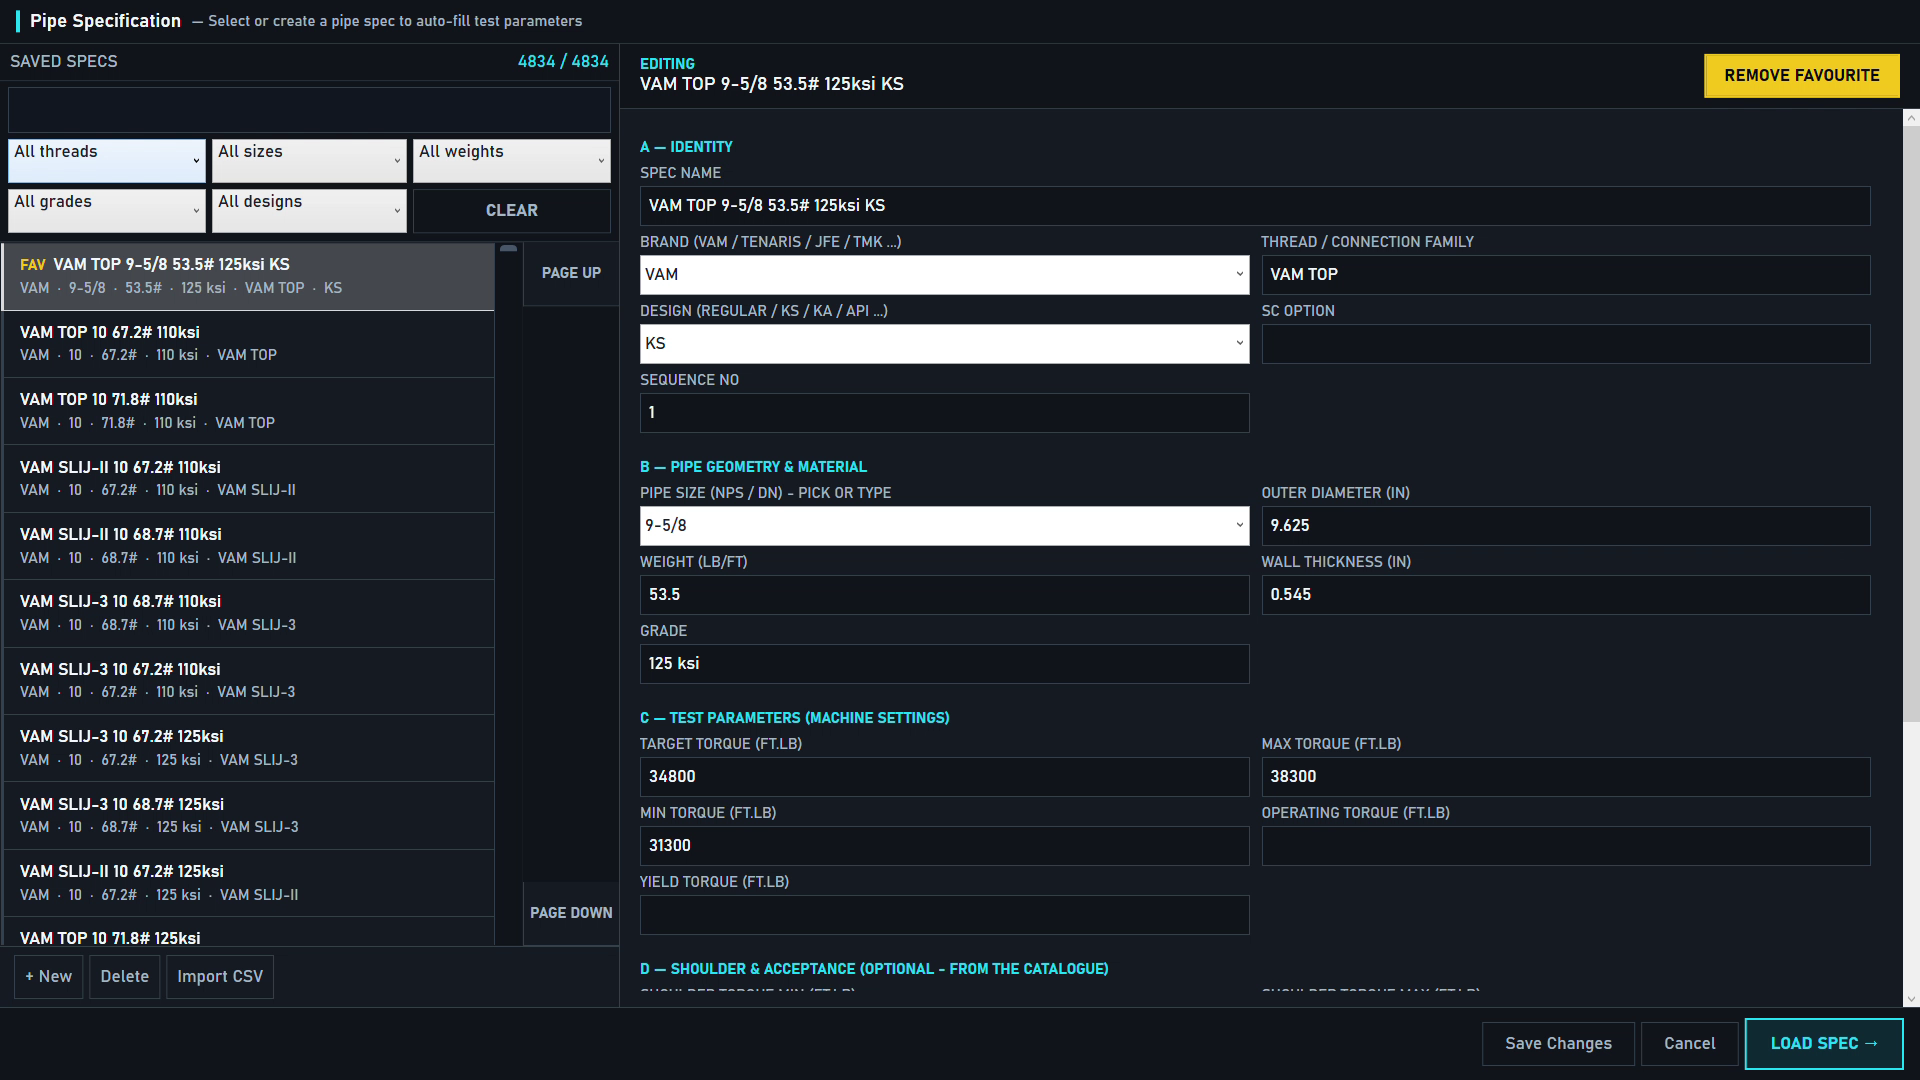
- Select by family, pipe size and grade; check weight, design and options.
- View minimum, target and maximum make-up torque.
- Where listed: shoulder, delta-turn and slope limits, plus clamping pressure.
Open full-size image ↗

Example from a separate make-up run.
Open full-size image ↗
Why we use Beckhoff control on our bucking unit
We choose Beckhoff for its PC-based platform, which can bring machine control, measurement and TorqueStar software together. That integration gives us flexibility to build the control and recording functions around your connection work.
| Why we choose it | What Beckhoff enables | What it means for your workshop |
|---|---|---|
| Control and software together | Machine control and custom operator software can run on one compatible industrial PC. | Connect TorqueStar’s connection selection, live curves and individual joint reports in one operating workflow. |
| Torque matched to turns | Optional measuring modules record when each reading was taken. | Match torque to the corresponding turn to review where the load rises and the connection shoulder forms. |
| A configurable tightening sequence | TwinCAT can be programmed to control hydraulic valves, speed changes and stopping. | Configure run-in, slower final tightening and stopping to suit the connection procedure, then verify them on the machine. |
| Room for additional requirements | Modular sensor inputs and software connections support expansion. | Plan for extra sensors or a connection to your production-reporting system when your work requires it. |
Platform details: TwinCAT · EtherCAT I/O · Measurement timestamps
From order confirmation to after-sales support
Before you order: confirm the machine
We review your connections and workshop requirements, then confirm the drawings, functions, configuration and supply scope with you before ordering. Acceptance requirements and service arrangements are agreed at this stage.
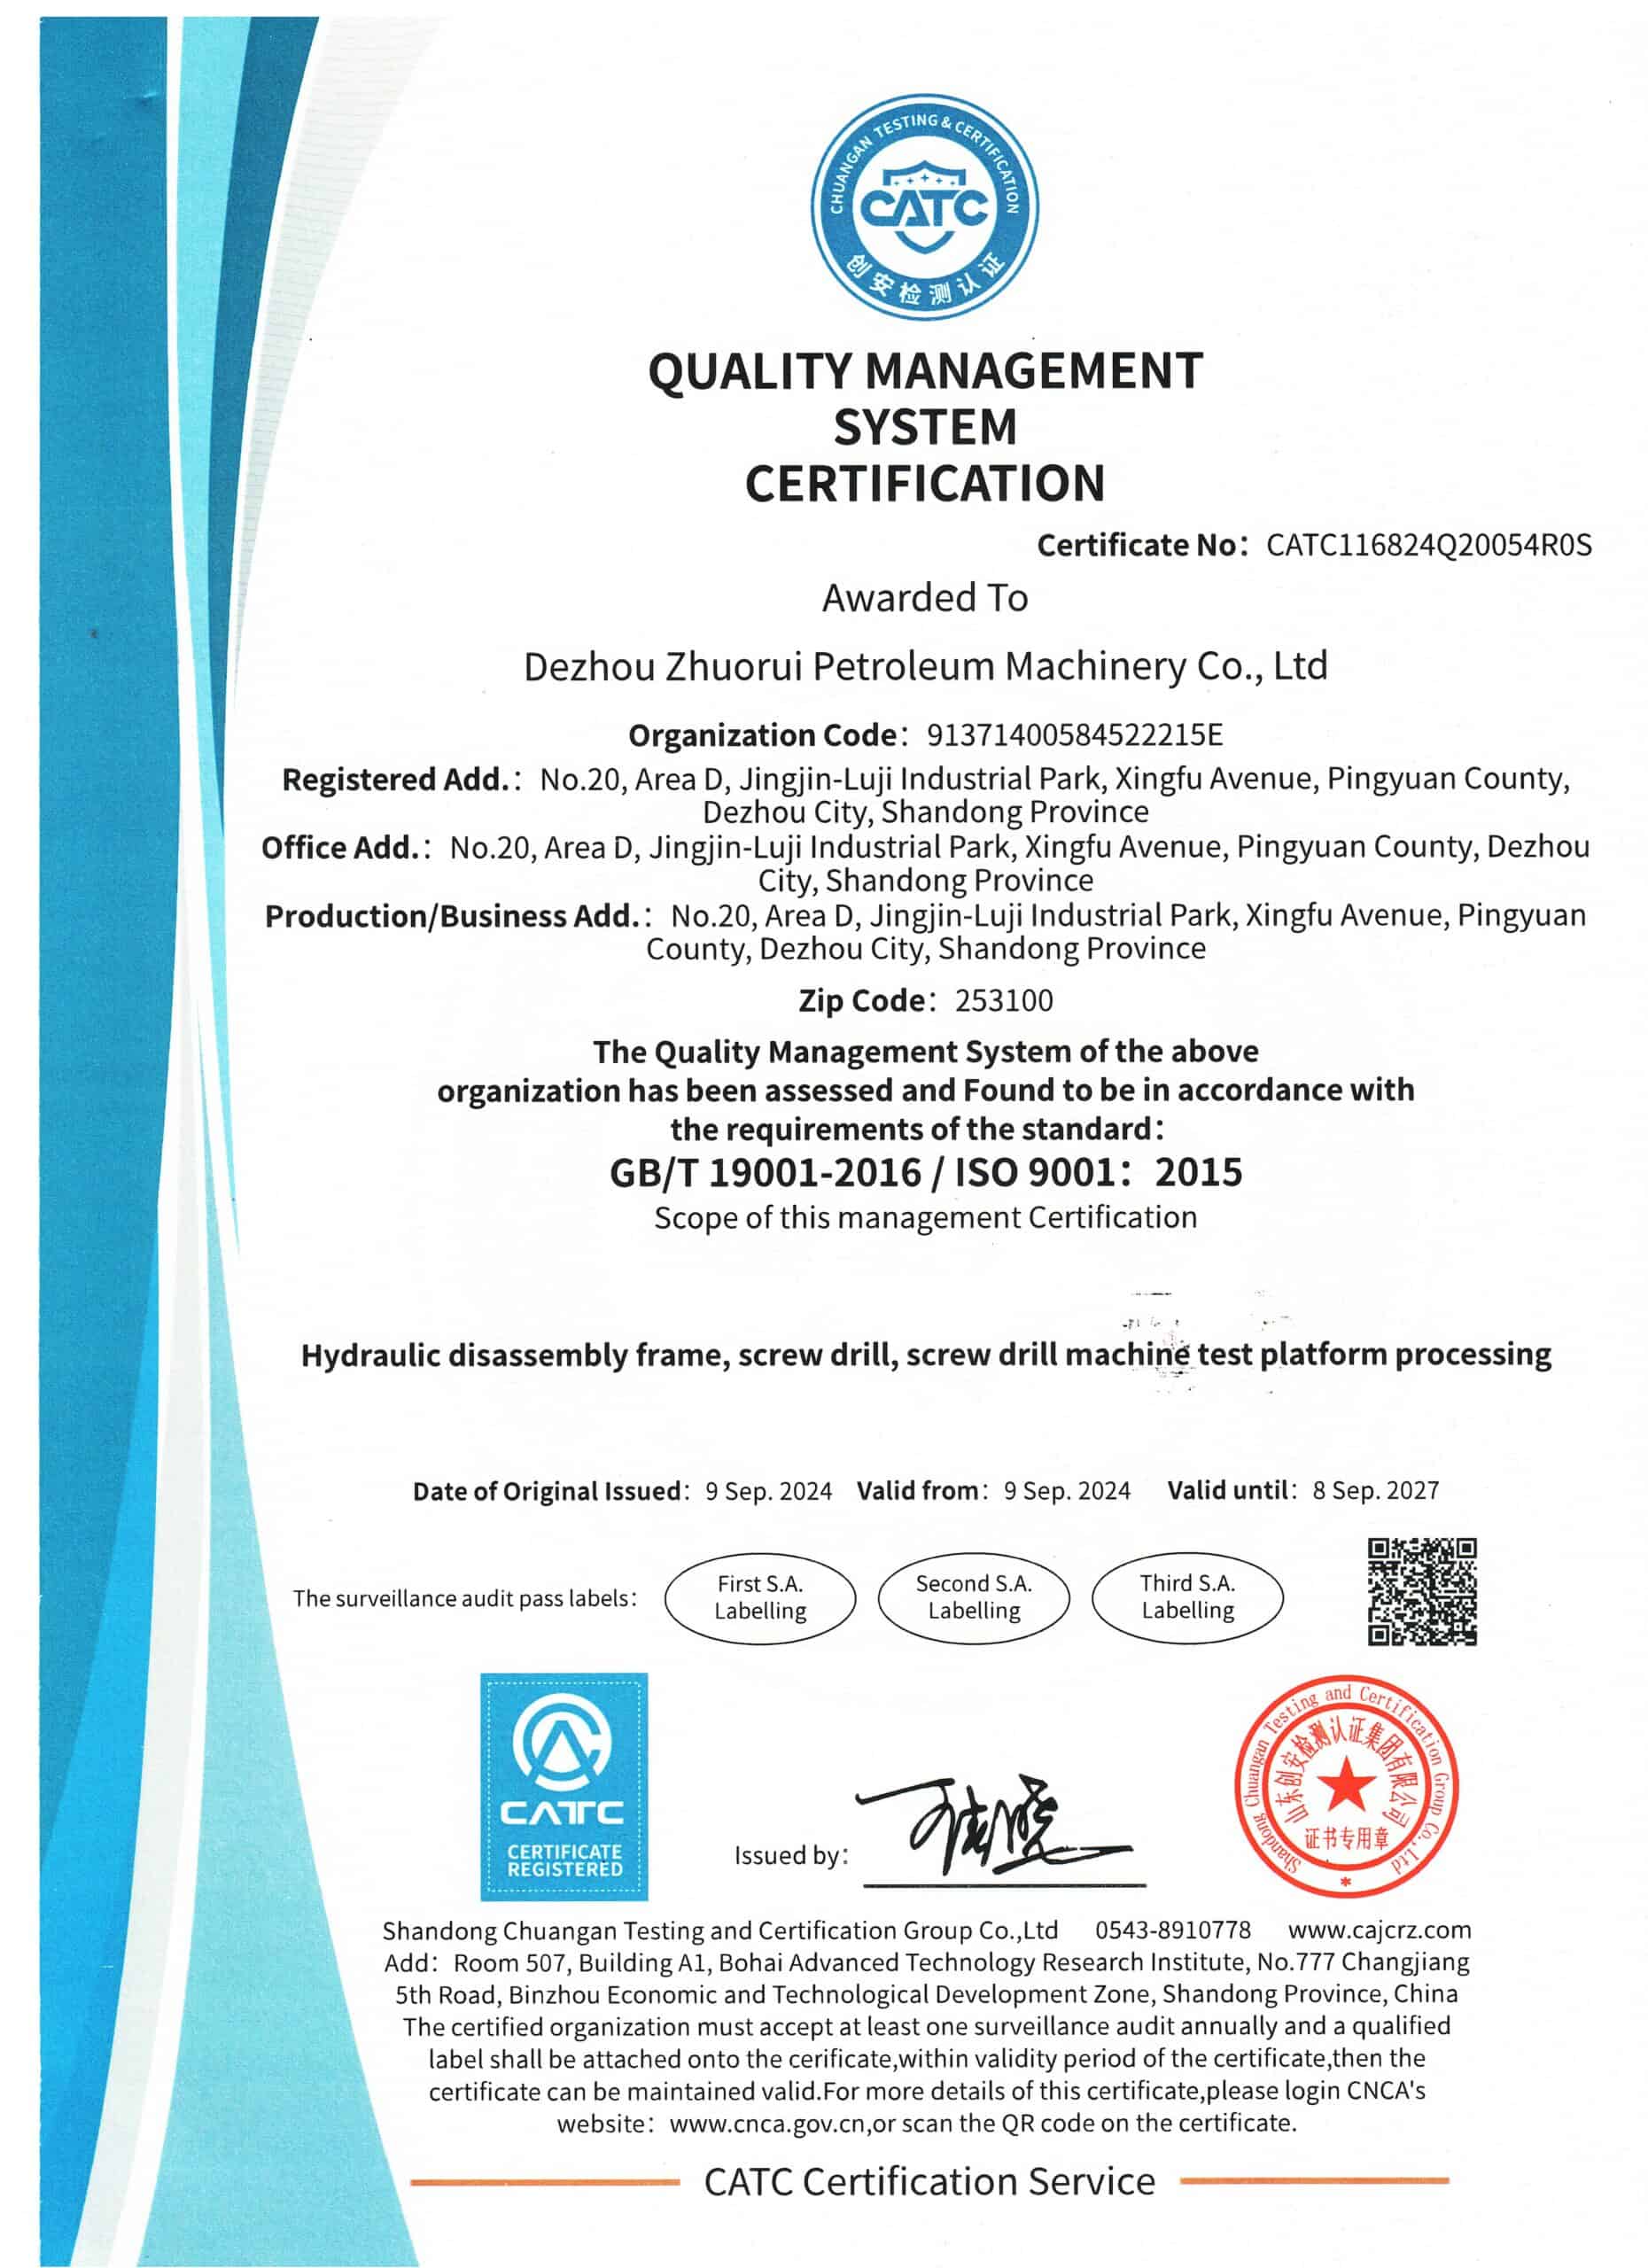
ISO 9001:2015 certified quality management
Our quality management system is certified to GB/T 19001-2016 / ISO 9001:2015. Certificate No. CATC116824Q20054R0S was awarded to Dezhou Zhuorui Petroleum Machinery Co., Ltd by Shandong Chuangan Testing and Certification Group and is valid until 8 September 2027.
Its certified scope reads “Hydraulic disassembly frame, screw drill, screw drill machine test platform processing”: our hydraulic breakout frames, screw drills and screw drill test benches. You can check the certificate number on the CNCA website (www.cnca.gov.cn).
Before shipment: witness the FAT
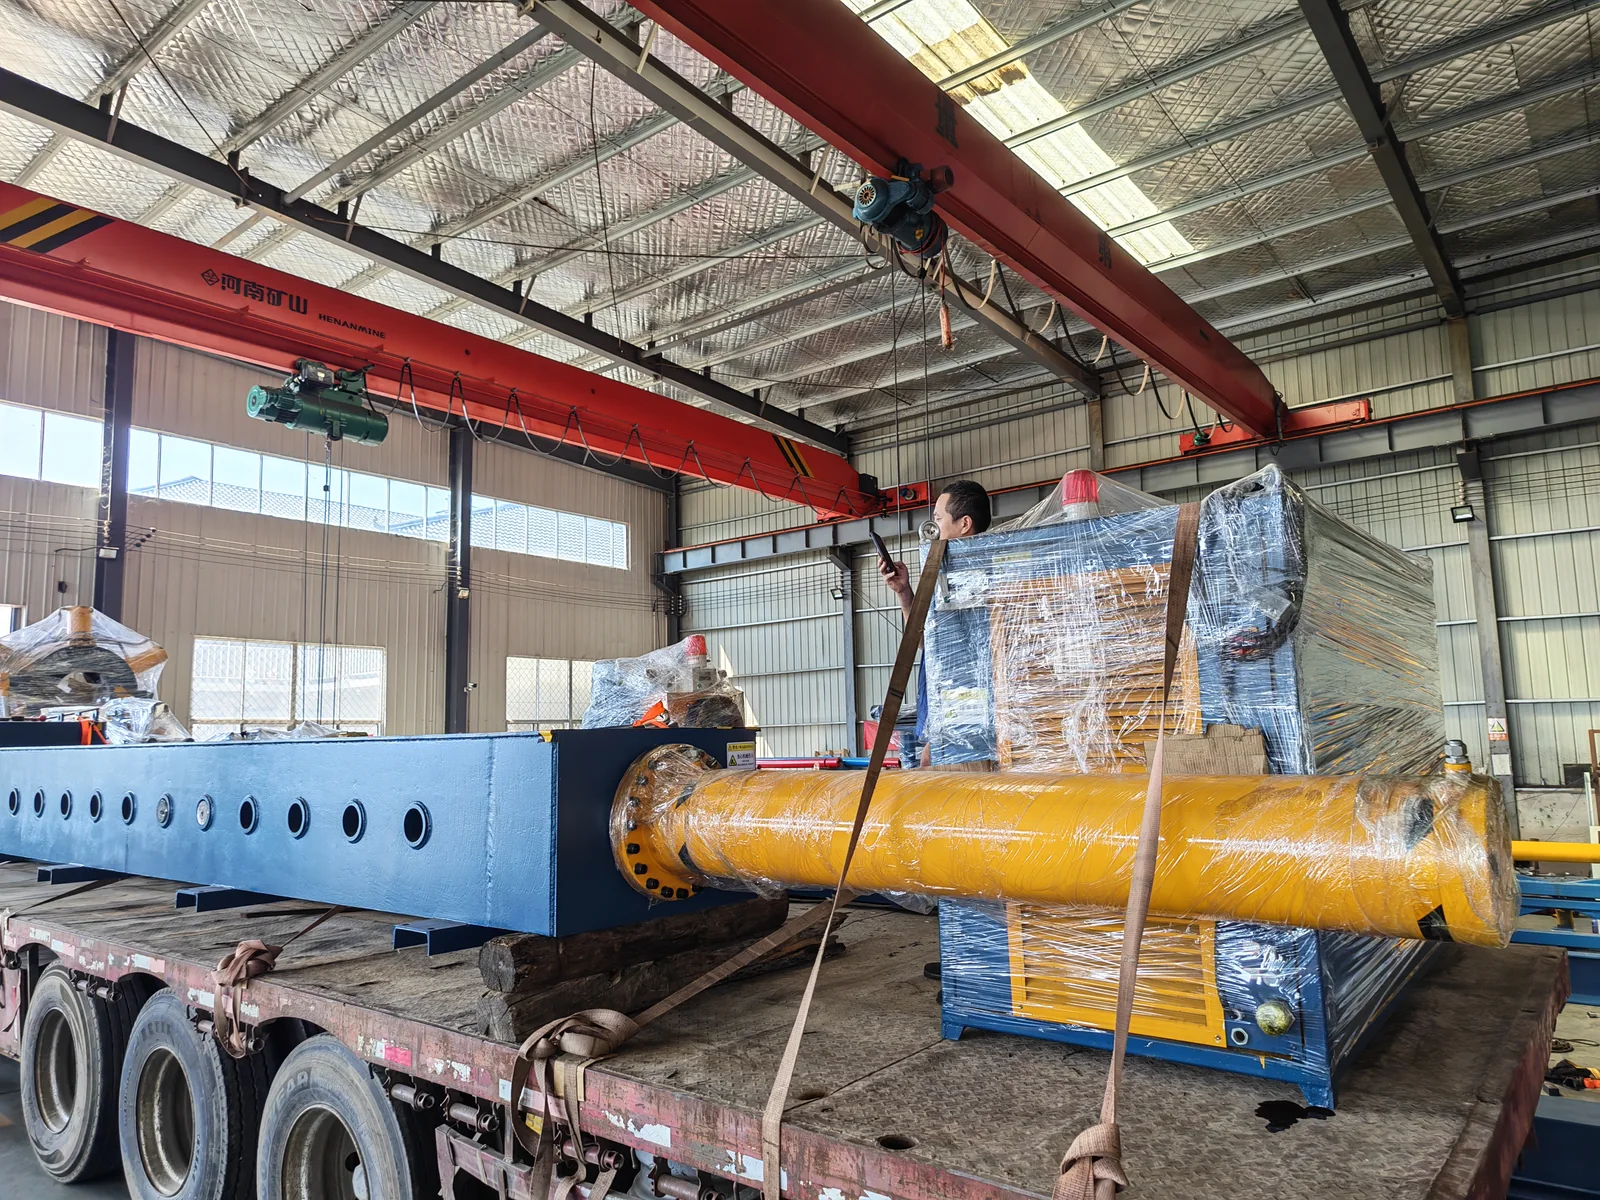
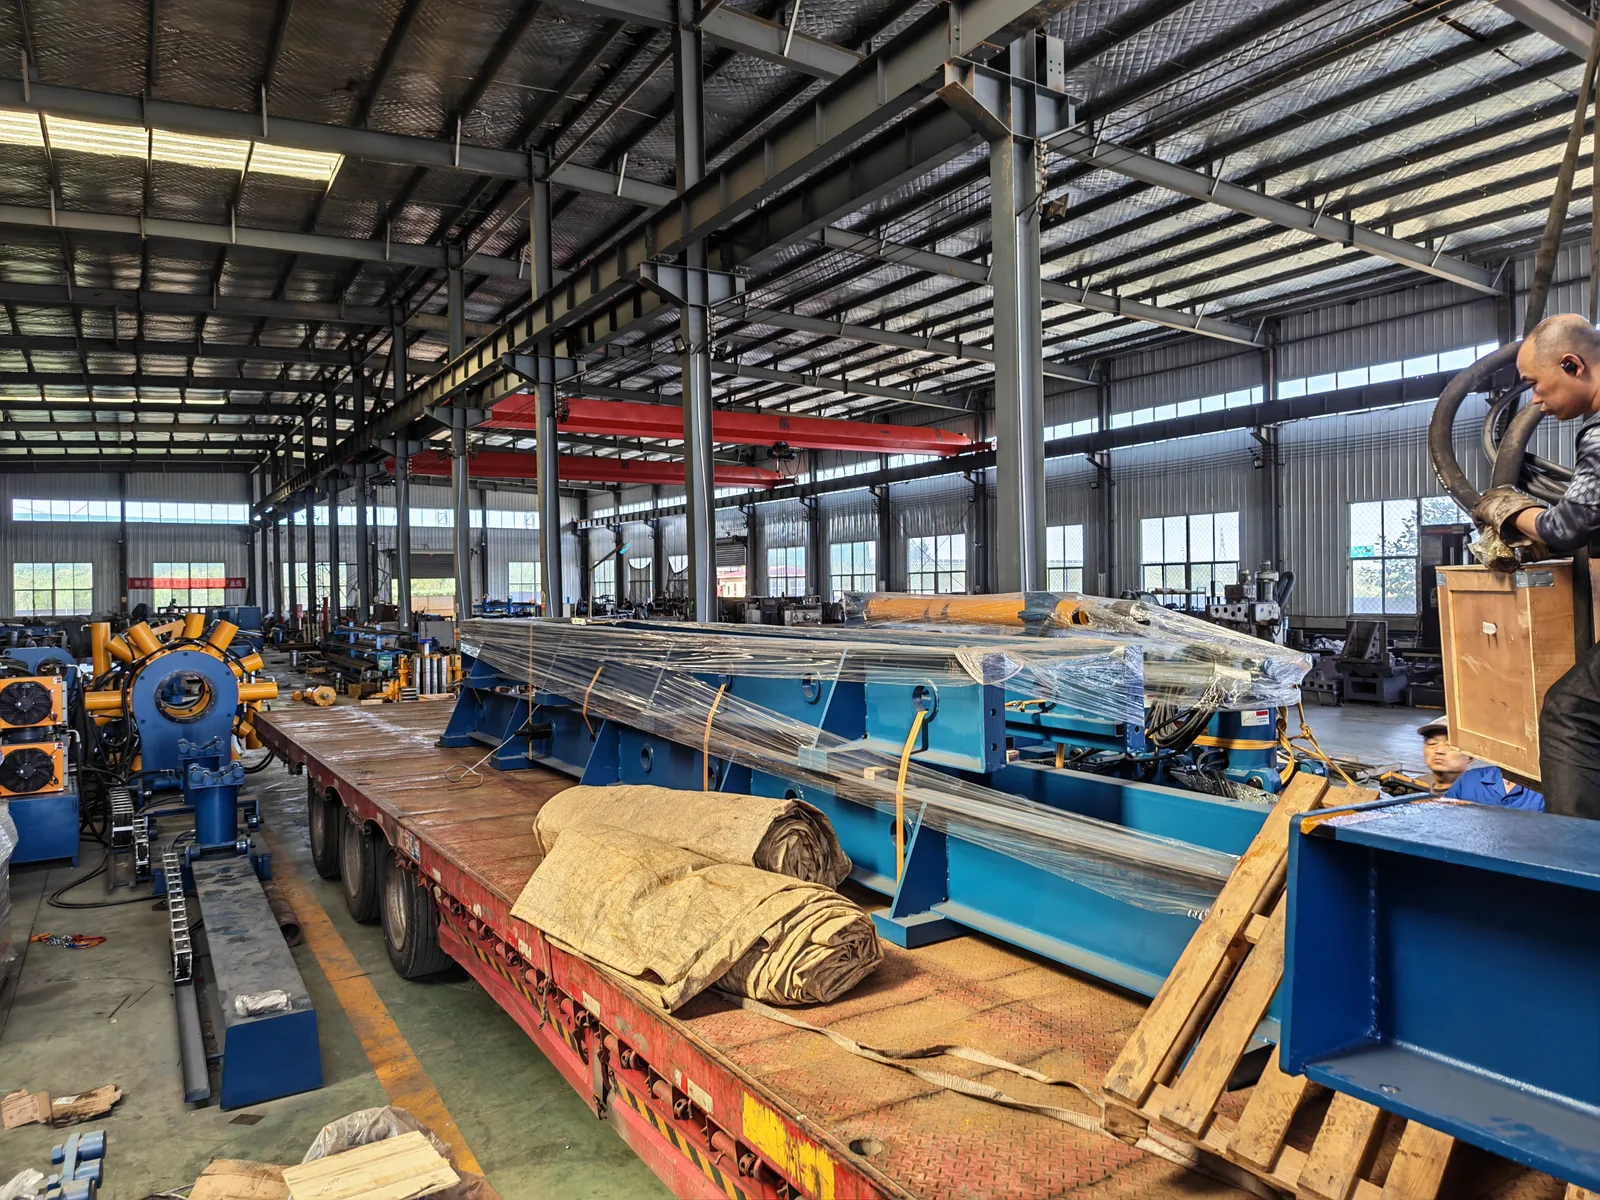
Once the machine is finished, we arrange a factory acceptance test (FAT) at our factory. You or your representative can attend, inspect the completed machine and test the agreed functions with our team before shipment.
The test follows the drawings, configuration and acceptance requirements confirmed before ordering.
Payment: T/T and L/C accepted
We accept T/T (bank transfer) and L/C (letter of credit). Advance payment depends on stock availability and the required configuration.
- In stock and ready for immediate testing: no advance payment is required.
- To be built or configured: advance-payment requirements and the payment schedule are agreed in the quotation.
The quotation confirms stock availability and when each payment is due.
After delivery: commissioning, training and support
- 18-month standard warrantyExtended coverage up to 3 years by written agreement.
- On-site commissioning & trainingAfter delivery, an engineer visits your workshop to commission the machine and train your operators.
- Remote technical supportHelp with operation and troubleshooting. Share the machine ID and alarm details.
- Spare-parts supportParts matched using your machine serial number and a part reference or photo.
- Whole-machine torque calibrationCalibration of the complete machine using torque transmitters and supporting calibration equipment.
- Middle East partner supportCalibration and after-sales support can be arranged through our regional partner. Tell us your machine model and location.
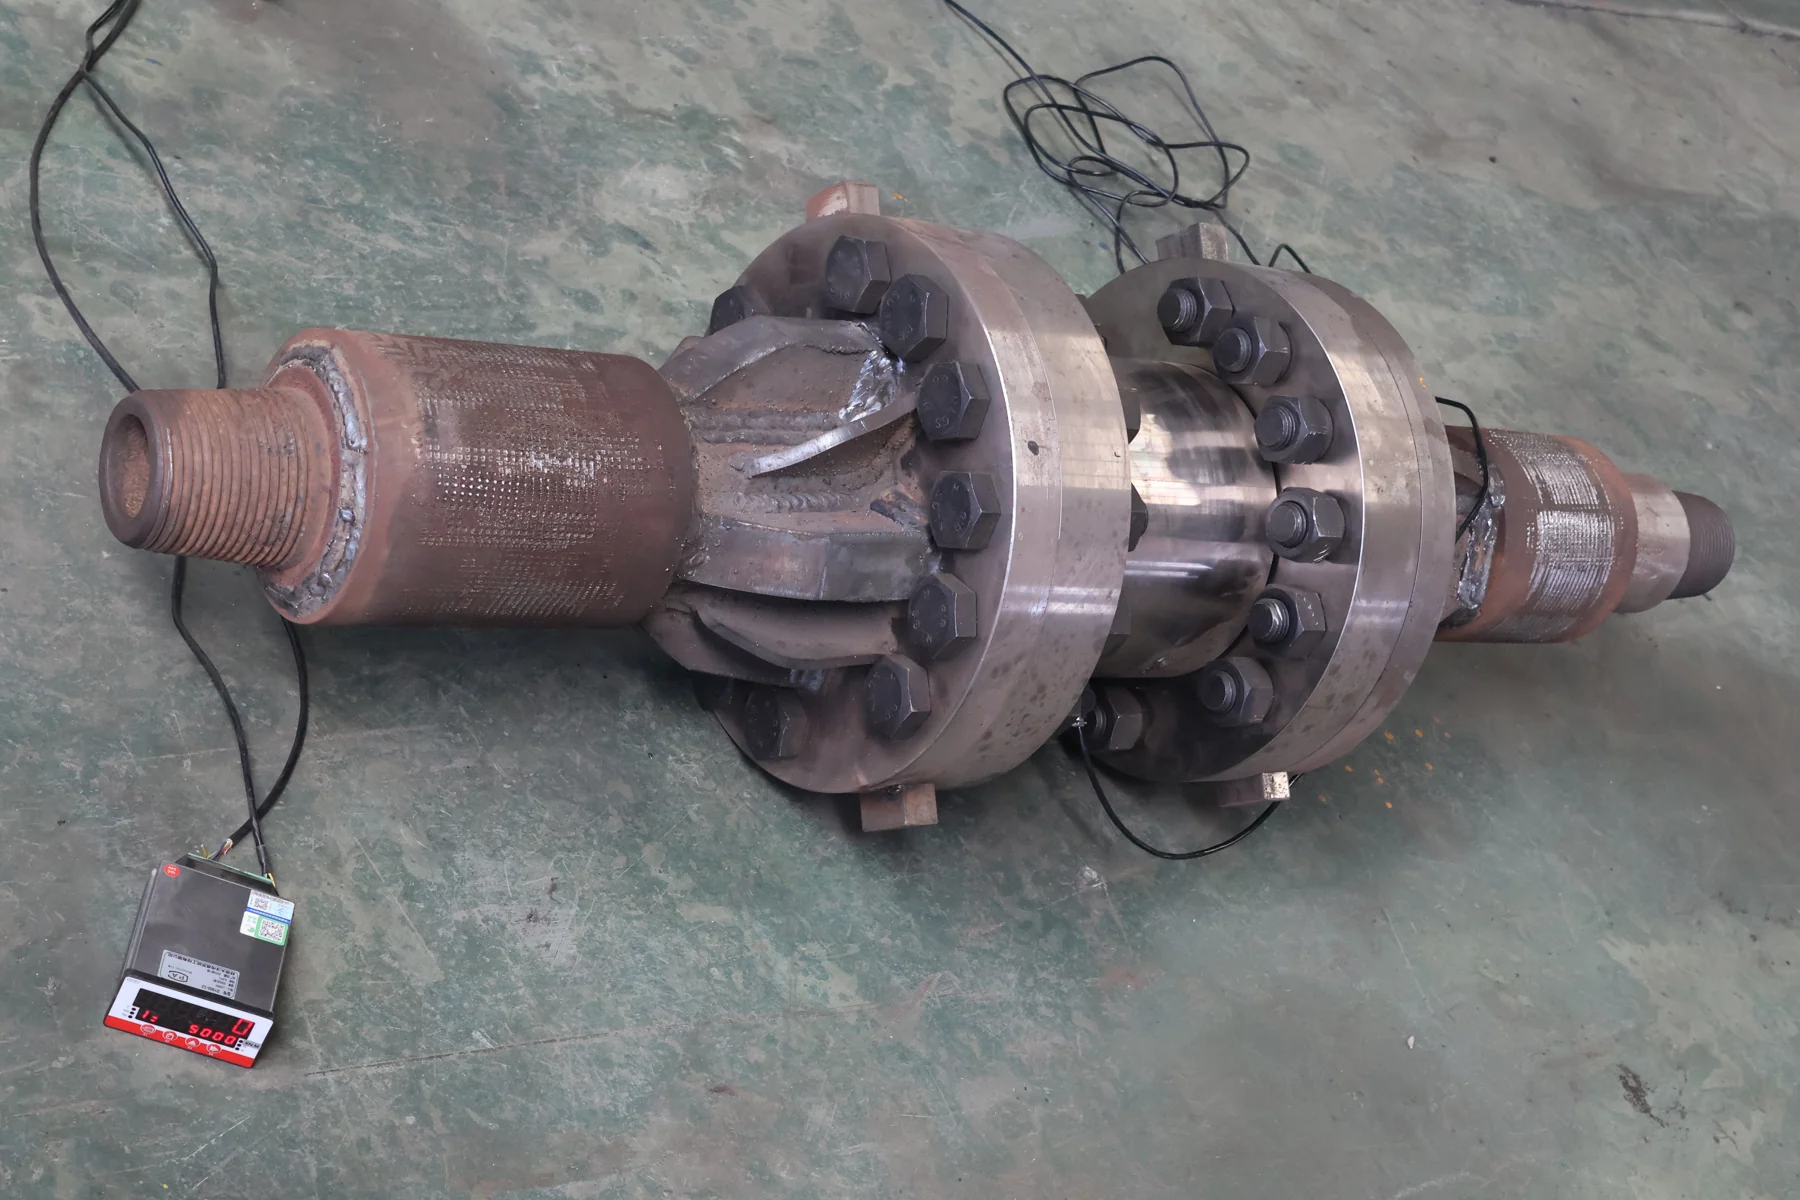
View calibration equipment ↗
Get a bucking unit quote
Share your connection, tool dimensions or the job you need to do. You can leave detailed specifications for the follow-up.
Send your requirements directly to Zhuorui. Read our privacy notice.
What is a bucking machine?
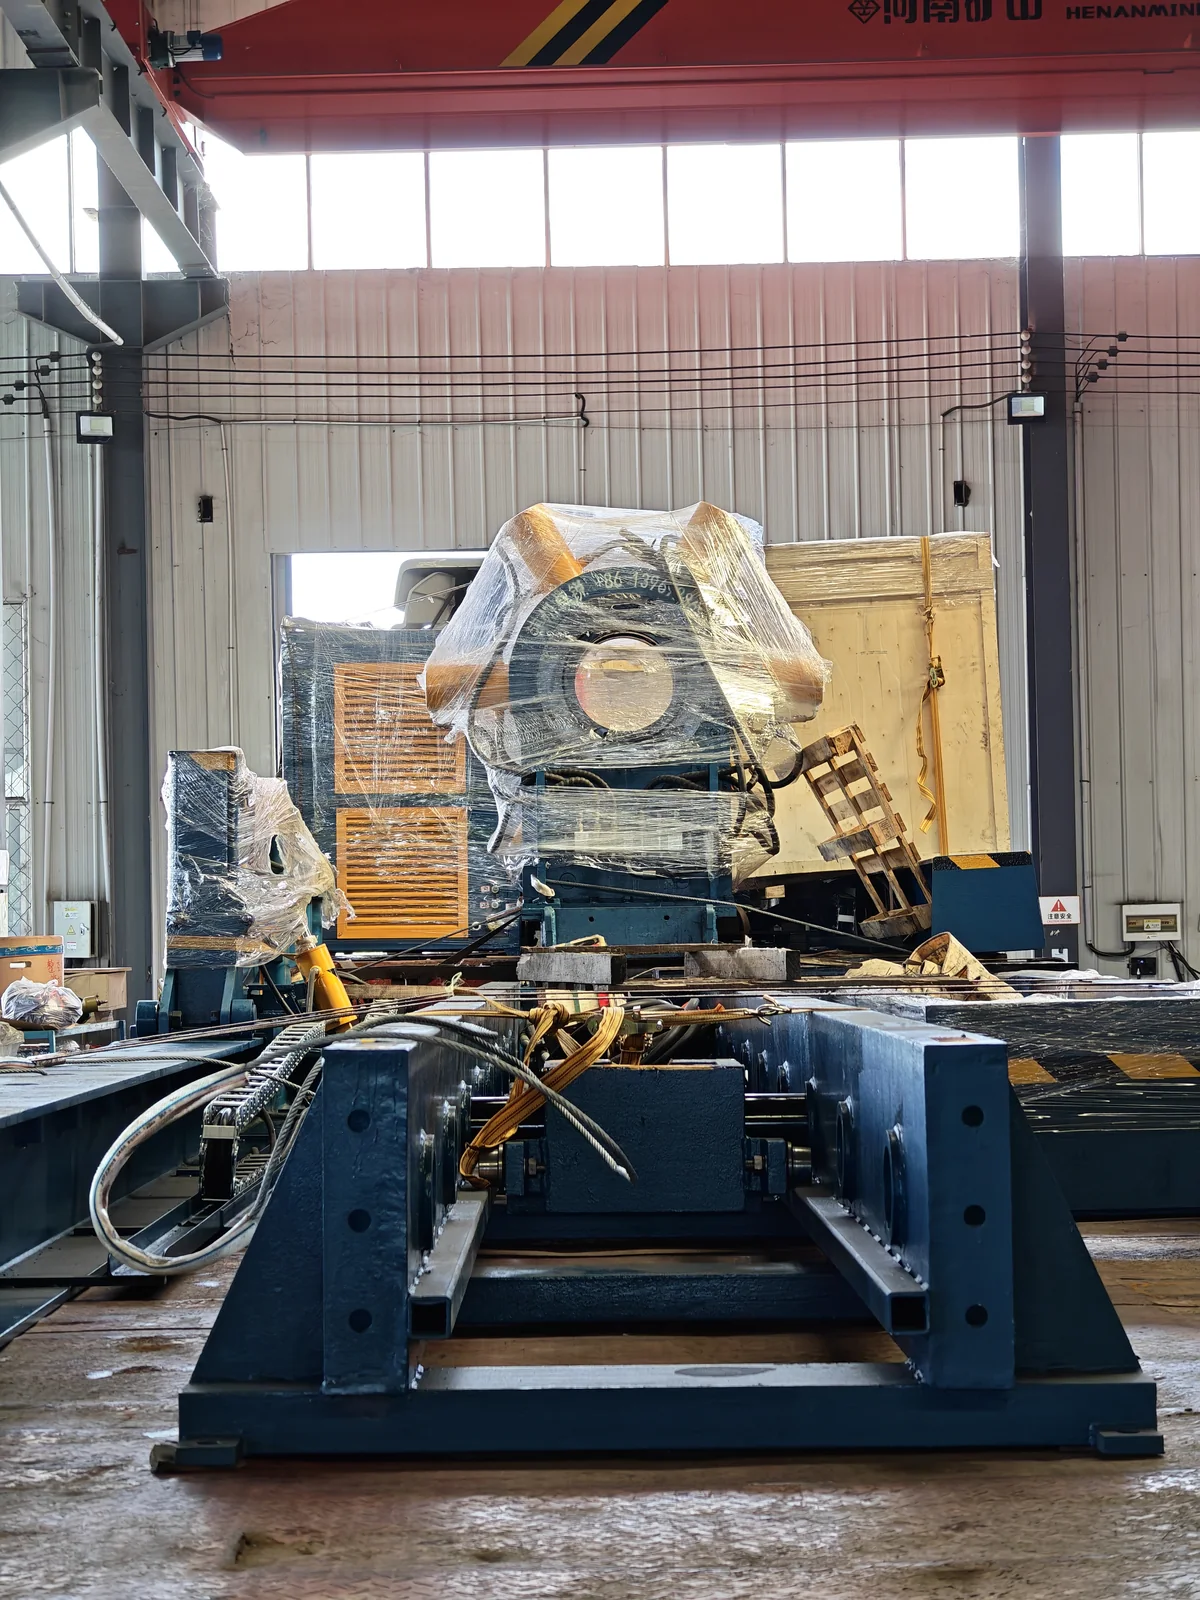
A hydraulic bucking unit, also called a pipe bucking machine, turns one part of a threaded connection while a backup head holds the other. Supports keep the assembly on the machine axis. Continuous rotation covers the initial thread run-in and the final make-up torque. The recording system plots torque against turns so the completed joint can be reviewed.
We supply configurations for casing, tubing, drill pipe, coupling buck-on (making up a coupling onto the pipe end) and downhole tools. For pipe make-up work, the combination of continuous rotation and a torque-turn record helps the workshop review each joint. If most of your work is dismantling service tools, compare the gripping and handling arrangements on our hydraulic breakout units.
Zhuorui is a bucking unit manufacturer in Dezhou, China. Established in 2011, the company carries out machining, hydraulic assembly and functional checks at its Pingyuan plant. Bucking units receive load testing, with torque-turn records supplied with the machine.
Bucking unit or breakout unit?
Both machines can make up and break out connections. Compare the drive, measured data and handling arrangement, rather than treating the names as opposite operations.
| Compare | Continuous-rotation bucking unit | Hydraulic breakout unit |
|---|---|---|
| Drive arrangement | A powered head turns continuously through 360° under torque. | High-torque wrenching and lower-torque thread spinning are separate functions. |
| Speed rating | Reference operating speed: 0.5-6 rpm for controlled make-up. | Spinner speed: up to 100 rpm. This is not the speed at maximum break-out torque. |
| Measured record | Torque against turns; shoulder and post-shoulder analysis with the specified package. | Target and executed torque, a torque-time curve and a connection summary. |
| Typical workshop work | Casing, tubing, coupling and connections requiring torque-turn acceptance. | Mud motor and downhole-tool disassembly, repair and reassembly. |
Clamping, continuous rotation and torque-turn monitoring
Continuous rotation
The powered head can keep turning through the connection run-in. Depending on the controls supplied, the operator can use a faster initial rotation and a slower approach to final torque. The required speeds follow the connection procedure.
Jaws and gripping surfaces
Tell us where the jaws can contact the workpiece, the length available for gripping and whether jaw marks are acceptable. Those details determine the jaw profile, contact material and clamping arrangement. Tubulars with sensitive surfaces need a separate tooling check.
Torque-turn monitoring
The display shows the torque-turn curve as the joint is made up, together with the configured torque limits. Shoulder analysis is available where specified. The curve and shoulder information must be checked against the connection owner’s current acceptance procedure.
Supporting long or heavy assemblies
The bed, support jacks and extension beams can be arranged to suit the assembly. We also need to know how it will be lifted into place, which end enters the machine first and where the operator will work.
Typical workshop uses
Casing, tubing and OCTG connection work
Oil country tubular goods (OCTG) work includes casing, tubing, couplings and pup joints. A bucking unit makes up their threaded connections and retains a record for each joint. The jaws must suit the actual gripping surfaces.
Premium connection assembly
Review torque-turn curves and the approach to the connection shoulder, using the connection owner’s limits and the monitoring functions specified for the machine.
Drill pipe and downhole-tool assembly
Assemble or separate drill pipe, BHA components and service tools that fall within the machine’s confirmed gripping, torque and support capacities.
Planning a connection job
- 01
Identify the connection
Provide the thread type, component drawing and current make-up procedure. Include the torque limits and the information you need in the joint record.
- 02
Choose the tooling and settings
The jaws, supports and control settings need to match the job before the operator starts the approved cycle.
- 03
Monitor make-up
The display follows torque and turns during make-up. A machine supplied with automatic control uses the programmed settings as it approaches the target torque.
- 04
Check the joint record
Compare the recorded curve and final values with the connection criteria. Save the reviewed record with the joint identification and job reference.
This sequence explains the work to plan for. Operators must use the approved machine instructions and the procedure for the connection being assembled.
Match the bucking unit to your connections
Start with the work you need to complete. Send a list of representative connections or tool drawings, including the smallest, largest, shortest and heaviest items. We can then review the gripping, torque, supports and recording requirements together.
| Your requirement | What to share and confirm |
|---|---|
| Connections and workpieces | Share connection families, pipe sizes, weights, grades and drawings. Identify the jaw contact areas and any limits on surface marking. Confirm the gripping range and dies for those actual surfaces. |
| Torque duties | State make-up and break-out torque separately, with units. Include the connection supplier’s procedure. Confirm both duties for the proposed configuration, including the lowest torque you need to measure. |
| Length, weight and handling | Give the longest and heaviest assembly, short pup joints and your loading method. Confirm bed length, support positions, lifting access and the room needed around the machine. |
| Controls and records | Specify manual or automatic operation and the records your customer requires. Review the Beckhoff PLC model, operator sequence, TorqueStar functions and a sample report against that requirement. |
| Workshop installation | Provide the installation country, voltage, frequency and a floor plan. Confirm the electrical load, hydraulic equipment, foundation requirements and who supplies each site connection. |
| Order and support scope | Before ordering, confirm the machine drawings, functions, configuration and itemized supply scope. Agree the after-delivery commissioning and training, calibration service, recommended spares and written warranty terms. |
Software and reporting requirements
Send your connection families, sizes, weights and grades so we can confirm the required library entries and acceptance fields with the software package. Specify torque-turn measurement, shoulder detection, PDF reports and CSV sample data as needed. The SD example shown here includes a shoulder marker, turns after shoulder and slope data. Measurement functions depend on the supplied sensors and software; speed reduction and automatic stopping also require the matching machine controls.
For the workshop file, agree the joint or tool identifier, operator name and job reference in advance. Review the curve and the acceptance criteria with the result, then save the report for that connection.
Read the workshop records guide →Agree what the factory acceptance test will demonstrate
We arrange the FAT at our factory on the finished machine before shipment. You or your representative can witness and participate in the test. Before ordering, choose representative connections and agree which functions and records the test must demonstrate.
- Fit and handling: demonstrate the agreed gripping arrangement, workpiece supports and operating sequence.
- Torque and recording: agree the verification method, measurement references, connection settings and report format.
- Handover: list the operating and maintenance instructions, drawings, software backup arrangements and spare-parts references required with the machine.
Bucking unit questions
How does this differ from a breakout unit?
Both machines make up and break out threaded joints, and manufacturers use the names differently. On this site, the bucking unit page covers continuous rotation and torque-turn assessment. The breakout unit page compares DZZR main torque, spinner ratings and tool-handling options. Choose by the connections and service work you need to perform.
Does frame size determine torque capacity?
No. The opening size, jaws, drive and hydraulic system all affect the usable capacity. The quotation should state both the gripping range and the torque duties, so you can check that they cover the same workpiece.
What is needed to assess a premium connection?
The connection owner’s current procedure sets the acceptance criteria. The machine needs the specified measurements and correctly configured limits. Torque-turn and shoulder data help with the review, but a common control setting cannot approve every premium thread.
What do you need for a quotation?
Send the minimum and maximum gripping diameters, connection drawings, make-up and break-out torque requirements, and the longest and heaviest assemblies. Include the workshop power supply, layout and an example of the report you need.
How do manual and automatic bucking unit controls differ?
With manual lever controls, the operator controls machine motion and follows the displayed measurements. An automatic control package can manage programmed parts of the cycle, including the approach to target torque. Specify who controls clamping, rotation and stopping at each stage; recording torque does not by itself make a unit automatic.
Can one bucking machine handle casing, tubing and drill pipe?
It can cover different tubulars when the gripping range, jaws, torque capacity and supports suit each assembly. Check the smallest gripping diameter as well as the largest connection. Include pup joints and short components in the review, because available clamping length can limit the setup.
How do I get a price for a bucking machine?
The quotation depends on the frame and gripping range, required torque duties, bed length, jaw sets and control package. Handling equipment, reporting functions and delivery scope also affect the total. Send a tool list and connection drawings through the bucking unit enquiry form for a configuration-based quotation.
Do you manufacture bucking machines for sale?
Yes. Zhuorui manufactures new hydraulic bucking units for pipe and tool connection work. Send your gripping dimensions, make-up and break-out torque requirements, and the records you need. We can then quote the machine, tooling and support package for your workshop.